 中文
 English
 Russian
 Thai
 Indonesian
 Vietnamese
 Portuguese, Portugal
 French
 日本
 Korean
 Hindi
 Spanish
 Turkish
 Arabic
 Bahasa Malaysia
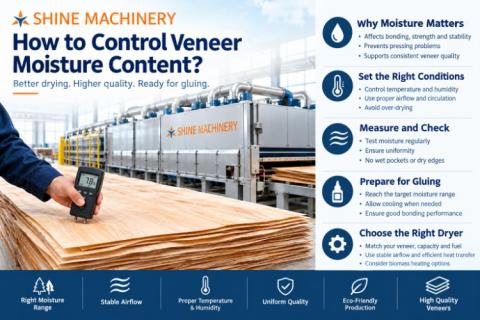
Controlling veneer moisture content is one of the most important steps in veneer production. Too much moisture can weaken bonding and create pressing problems. Too little moisture can make veneer brittle and difficult to glue.
We focus on moisture control because good drying supports stable veneer quality. The goal is simple: dry veneer evenly and prepare it for the next production step.
Why Veneer Moisture Matters
Moisture Affects Veneer Quality
Freshly peeled veneer contains a large amount of water. The drying process must remove that water without damaging the wood. Research shows that moisture content affects bonding, strength, and dimensional stability.
In our experience, uniform moisture matters as much as the final number. A sheet with wet spots can cause trouble during gluing. Meanwhile, an over-dried sheet may become brittle or develop surface defects.
Match Moisture to the Application
There is no universal moisture target for every product. Decorative face veneer often reaches about 8%–10%, while commercial hardwood veneer for urea glue often uses 6%–8%. Some plywood processes target lower levels, depending on the adhesive and production method.
Therefore, we always consider:
- Wood species
- Veneer thickness
- Adhesive type
- Final product
- Pressing conditions
- Required moisture range
Control Drying Conditions
Set the Right Temperature
Temperature strongly affects the drying process. Higher temperatures can shorten drying time, but excessive heat can change veneer color and surface properties. One study found higher drying temperatures increased surface roughness and color change.
We recommend starting with the material, not the machine setting. Thin veneer usually needs less drying energy. Dense hardwood may need more controlled drying conditions.
Balance Temperature and Humidity
Temperature alone cannot control moisture accurately. Hot and humid air moves through the veneer and carries moisture away. Air temperature, humidity, speed, and circulation all influence drying performance.
We monitor these factors together. This approach helps us avoid sudden drying and uneven moisture loss. In short, the air needs to work with the wood, not fight it.
Improve Veneer Drying
Use Proper Airflow
Good airflow helps heat reach the veneer surface evenly. It also removes moist air from around the veneer sheets. Poor circulation can leave some sheets wet while others become too dry.
A properly designed dryer keeps air movement stable across the drying section. This helps create more consistent moisture results throughout production.
Avoid Over-Drying
It sounds strange, but drier does not always mean better. Excessive drying can reduce bonding performance and affect veneer appearance. Studies have reported changes in bonding and surface properties at higher drying temperatures.
We therefore aim for the required moisture range rather than the lowest possible number. Wood is not a potato chip. We do not want it dry just for the sake of being dry.
Measure Moisture After Drying
Check Moisture Content Regularly
A reliable moisture meter helps operators track the drying result. We recommend checking samples from different parts of the production line. This can reveal differences between the dryer entrance, center, and exit.
The USDA Forest Products Laboratory notes that plywood plants can measure sheets as they leave the dryer. Operators can then re-dry sheets that remain too wet or condition sheets that become too dry.
Watch Moisture Uniformity
Average moisture content does not tell the whole story. Two veneer sheets may show the same average value but behave differently during gluing.
For this reason, we look for:
- Stable average moisture
- Small moisture variation
- No obvious wet pockets
- No severely over-dried edges
- Consistent results between batches
Prepare Veneer for Gluing
Reach the Target Before Glue Spreading
The final target should match the adhesive system and product requirements. Properly dried veneer becomes ready to be glued when its moisture level falls within the required range.
Research has found that excessive veneer moisture can contribute to poor bonding and even steam-related defects during hot pressing.
After drying, we also allow veneer to cool when the production process requires it. This gives the sheets better conditions for accurate glue application.
Use the Right Drying Equipment
Choose a Dryer for Your Veneer
A suitable Veneer Dryer Machine should match your veneer thickness, species, production capacity, and fuel system. Roller dryers work well for many plywood core veneers. Mesh-belt systems can suit delicate or thin face veneers.
At Shine Machinery, we focus on stable airflow, controlled heat transfer, and practical production capacity. We also consider biomass heating options when customers want to reduce dependence on fossil fuels.
The right system makes moisture control easier. More importantly, it helps producers create high quality veneers with consistent results.
Final Moisture Control Checklist
Before sending veneer to gluing, we suggest checking these points:
- Moisture: Within the target range
- Uniformity: No major wet or dry areas
- Temperature: Suitable for the next process
- Airflow: Stable across the dryer
- Drying time: Long enough for the veneer thickness
- Wood species: Considered during setup
- Adhesive: Matched to the moisture target
- Quality: No serious cracks, burning, or brittleness
Good moisture control does not come from one setting. It comes from balancing temperature and humidity, airflow, drying time, and regular measurement. When these factors work together, veneer becomes more stable, more consistent, and ready to be glued.
For modern veneer drying, we believe consistency matters most. A well-controlled drying line protects veneer quality while supporting efficient and reliable production.
- Войдите или зарегистрируйтесь, чтобы оставлять комментарии